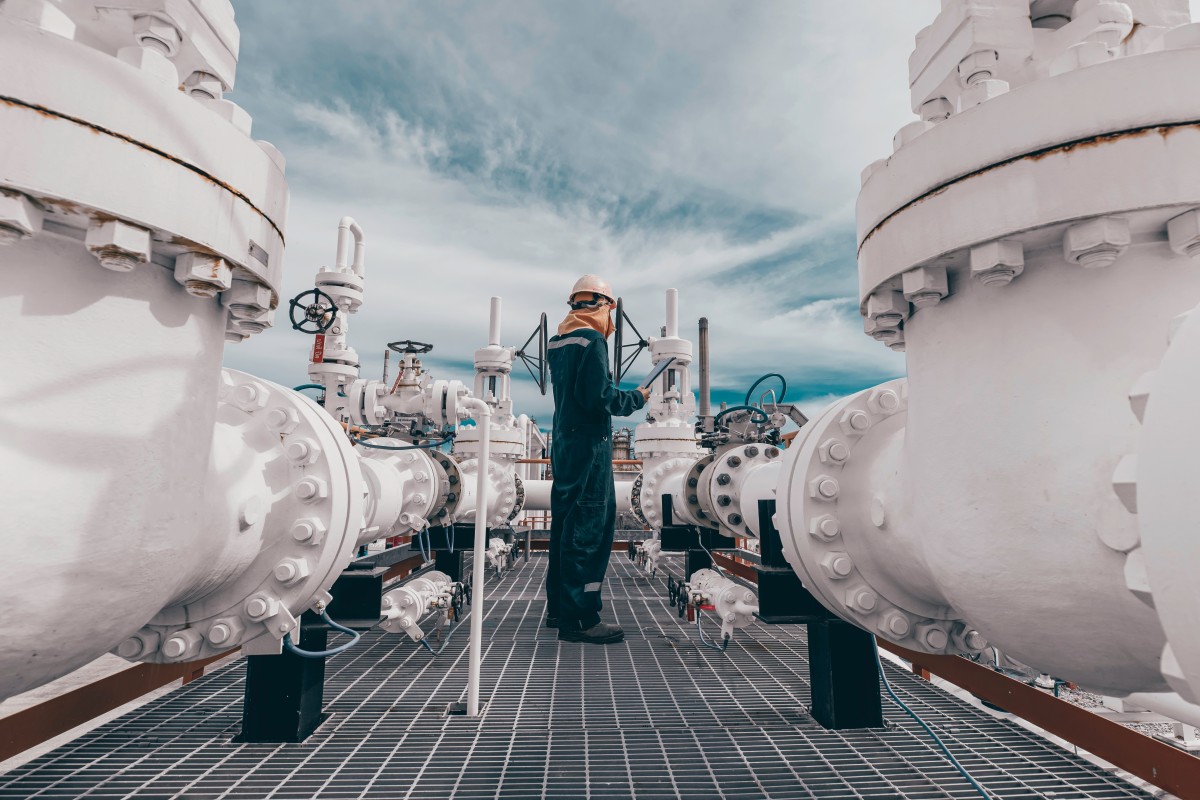
Above: Sealing reliability is becoming increasingly critical as industrial valve systems face higher pressures, wider temperature swings and more aggressive operating environments. Image credit Shutterstock
Sealing reliability is no longer determined solely by valve design or maintenance discipline. As hydrogen, carbon capture and increasingly aggressive process conditions push equipment beyond traditional limits, material science is becoming critical to long-term integrity, emissions control and uptime.
By: Tyler Monzel, Global Product Manager – Sealing Systems, Greene Tweed
Industrial valve systems are facing operating environments that would once have been considered exceptional. Higher pressures, wider temperature swings, aggressive chemicals, hydrogen transport, carbon capture infrastructure and increasingly demanding efficiency targets are redefining what operators expect from sealing systems. Simultaneously, minor leaks, once accepted as an operational reality, now carry major commercial, environmental, and operational safety consequences.

Arlon® 3000XT components are designed to support dimensional stability and leak-tight performance in high-pressure, high-temperature sealing applications
This shift is changing the engineering conversation from valve geometry and mechanical design to the fundamental properties of materials that decide performance, durability, and efficiency under extreme conditions.
The challenge is especially acute across severe-service valves, pumps and compressors operating in energy, petrochemical, offshore and emerging hydrogen applications. Equipment is now routinely exposed to conditions that push traditional elastomeric materials, including standard NBR and FKM, beyond their design limits. These materials were not designed for supercritical CO2, hydrogen permeation, deepwater pressure profiles, or aggressive modern chemical streams. Temperature alone is no longer the defining factor. Instead, pressure cycling, chemical exposure, decompression events and media permeation combine to place far more complex demands on sealing systems.
As a result, long-term sealing performance is now determined by how materials behave over time under real operating conditions. A seal may perform perfectly during installation and initial commissioning, yet fail prematurely if the material experiences swelling, thermal hardening, chemical degradation or compression set after prolonged exposure in service. This changes the financial equation around material selection.
The lower upfront cost of a conventional material can be outweighed quickly if degradation leads to early replacement, unplanned intervention, production loss or compliance exposure.
This distinction between initial sealing performance and long-term material stability is becoming increasingly important in industries where downtime carries significant operational cost. The issue is not simply whether a seal works when first installed, but whether it continues to maintain integrity after years of pressure cycling, chemical exposure and temperature fluctuation.
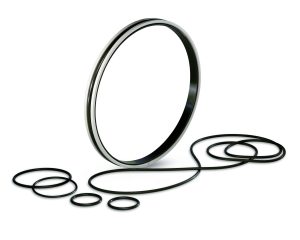
Greene Tweed’s Fusion® 938 fluoroelastomer is formulated for demanding sealing environments where rapid gas decompression, chemical exposure and thermal cycling can challenge conventional materials
The changing operating envelope
The evolution of industrial energy systems is accelerating the problem. Hydrogen infrastructure, carbon capture projects and deeper offshore developments are introducing operating conditions that expose weaknesses in traditional sealing strategies. Hydrogen is especially demanding because it combines an exceptionally small molecular size with extreme operating conditions. Liquid hydrogen is stored at cryogenic temperatures of approximately -253°C, while compressed gaseous hydrogen is commonly stored at pressures ranging from 250 to 350 bar in industrial applications and up to 700 bar in transportation and other high-pressure applications. These conditions intensify the combined challenges of permeation, pressure cycling and rapid gas decompression, requiring seals to maintain integrity across wider operating extremes than many conventional elastomers were designed to handle.
During decompression, hydrogen trapped within the elastomer expands rapidly as pressure falls, potentially causing blistering, cracking and catastrophic structural failure within the seal itself.
Rapid gas decompression (RGD) is becoming one of the defining sealing challenges in modern hydrogen and carbon capture infrastructure. The problem is especially severe in hydrogen and supercritical CO2 applications, where gas molecules can permeate deeply into sealing materials under pressure. When decompression occurs, the trapped gas must escape rapidly. If the material structure cannot tolerate that expansion, the seal effectively fails from within.
Traditional materials frequently struggle under these conditions because they were never designed for sustained exposure to such aggressive decompression cycles. Material formulation therefore becomes critical. Compounds engineered specifically for RGD resistance can dramatically improve reliability by maintaining structural integrity during decompression events that would destroy standard elastomers.
While much of the discussion around hydrogen sealing has focused on elastomeric materials, they are only part of the challenge. Hydrogen’s combination of cryogenic temperatures, high operating pressures and repeated pressure cycling also places significant demands on thermoplastic components used in critical valve systems, where long-term dimensional stability is equally important to maintaining sealing integrity.
One example is the demand placed on thermoplastic components within hydrogen pressure relief systems. The thermoplastic seats in these pressure relief valves for hydrogen and high-pressure gases often struggle with creep causing the material to deform over time. Even a small amount of creep can allow small hydrogen molecules to escape through the relief valve. To combat this, a Fortune 500 engineering solutions company has replaced its legacy valve seat materials with Greene Tweed’s cross-linked PEEK polymer, Arlon® 3000XT.
Sealing components designed with Arlon® 3000XT have been designed and tested to maintain leak-tight performance at pressures exceeding 20,000 psi. A decade of field use and testing under high-pressure, high-temperature (HPHT) conditions have proven Arlon® 3000XT outperforms traditional materials like filled PEEK, making it ideal for gaskets, o-rings, and backup rings in hydrogen systems.
This development reflects a wider industry trend in which material selection is becoming central to achieving reliable containment in high-pressure hydrogen service. The challenges are not unique to hydrogen. Carbon capture and storage systems introduce their own material compatibility problems. For example, supercritical carbon dioxide can leach plasticisers from lower-grade elastomers, leaving materials brittle and vulnerable to cracking over time. Operators specifying seals for CCS systems must therefore consider decompression resistance, permeation behaviour and chemical compatibility simultaneously rather than treating them as isolated engineering concerns.
Traditional material selection practices are no longer sufficient for severe service environments. For engineers specifying seals in critical energy and process applications, nominal operating conditions alone rarely provide an accurate picture of real service exposure. Pressure spikes, thermal cycling, chemical variations, decompression events, and abnormal process conditions often create transient extremes that ultimately determine seal life.
This is particularly problematic in valve systems, where operators often specify according to steady-state operating conditions while underestimating the importance of transient events. A seal may tolerate standard operating temperatures without difficulty yet fail repeatedly during startup cycles, shutdown sequences or pressure excursions that momentarily exceed its thermal or decompression limits. These short-duration events are often what govern long-term reliability in harsh-service environments.
The same issue applies to chemical compatibility. Material selection has historically prioritised temperature and pressure capability, but operators are increasingly discovering that chemistry can rapidly undermine otherwise capable materials. Steam, amines, aggressive solvents and sour gas environments can soften, swell or embrittle elastomers far below their nominal temperature limits. A material capable of operating at 300°C in dry conditions may fail at half that temperature when exposed to aggressive process chemistry.

In severe service valve applications, seal material selection, geometry and system design all influence long-term leakage control, reliability and maintenance performance
Leakage is no longer acceptable
Environmental concerns are also reshaping the sealing conversation. Regulatory requirements to reduce fugitive emissions, together with broader ESG commitments, are forcing operators to reconsider how they approach leakage across process systems.
Leakage can now create exposure to penalties, remediation costs, production disruption and reputational risk, particularly as emissions reporting requirements become more stringent. That makes high-integrity sealing a risk-management decision.
Historically, many facilities treated minor leakage as a maintenance issue to be managed reactively. Increasingly, operators are viewing leakage as a design failure that should be engineered out of the system entirely.
That shift has major implications for material selection. Sealing technology effectively represents the front line of emissions control in valves, pumps and compressors. Without high-integrity sealing systems, long-term methane reduction targets or hydrogen containment strategies become extremely difficult to achieve consistently.
This is particularly relevant in remote and offshore environments where maintenance intervention itself carries enormous operational cost. A single unplanned maintenance event on an offshore platform may involve helicopter transport, lost production time and major operational disruption. An industry report estimates that offshore oil and gas organisations experience an average of 27 days of unplanned downtime per year, with average annual losses of around $38 million. While not all downtime is seal related, the figure illustrates why reliability decisions in these environments are increasingly viewed through a lifecycle-cost lens. In subsea systems or isolated process facilities, the total cost of seal failure can outweigh the price of premium sealing materials many times over.
As a result, operators are increasingly evaluating sealing systems according to lifecycle performance rather than initial purchase cost alone. The conversation is gradually moving away from whether higher-performance materials are more expensive towards how lower-performing materials can create unacceptable operational risk, increase maintenance requirements and inflate total cost of ownership over the life of the asset.
This lifecycle perspective is encouraging wider adoption of advanced polymer and composite-based sealing solutions designed for harsh-service applications. High-performance FFKM compounds, advanced PEEK composites and engineered thermoplastics are increasingly being specified where operators need extended maintenance intervals, lower leakage rates and greater reliability under severe conditions.
The benefits are not limited to chemical resistance. Advanced polymers can deliver combinations of wear resistance, thermal stability and low-friction performance that conventional materials struggle to achieve simultaneously. In dynamic valve and pump systems, this becomes particularly important because friction, galling and wear directly influence long-term equipment reliability.
Materials that extend equipment life
Composite wear components are now replacing metallic parts in many pumps and compressors because they can operate with tighter clearances while avoiding the galling and seizure risks associated with metal-on-metal contact. Operators adopting composite wear parts have reported reductions in vibration, lower power consumption and longer mean time between repairs.
The broader implication is that sealing and wear materials are no longer passive consumables within industrial systems. Material performance increasingly influences operational efficiency, equipment uptime and maintenance strategy across the entire asset lifecycle.
The transition towards advanced materials is especially visible in applications involving extreme chemistry. Perfluoroelastomer materials such as FFKM compounds are being adopted across refining, chemical processing and severe-service instrumentation because they combine the elasticity of elastomers with chemical resistance approaching that of PTFE.
These materials maintain physical properties in highly aggressive environments involving steam, solvents, acids, and pressure cycling where conventional elastomers degrade rapidly. Their ability to tolerate both extreme temperatures and aggressive media makes them extremely valuable in applications where seal failure risks contamination, emissions or production shutdowns.
In many cases, the operational improvements achieved through material optimisation are substantial. Analytical instrumentation manufacturers, for example, have extended seal life dramatically by moving from standard fluoroelastomer materials to specialised FFKM compounds capable of withstanding highly aggressive chemical exposure. In one case, seals that previously failed after only two testing cycles continued operating successfully across multiple reaction cycles without deterioration after a material change.
The same principle increasingly applies to industrial valve systems. Operators replacing standard FKM materials with advanced FFKM compounds in refinery and hydrocarbon processing applications have reduced fugitive emissions and significantly improved thermal cycling reliability. In severe-service valves, carefully selected composite and polymer materials have enabled maintenance intervals to extend from annual shutdown cycles towards multi-year operational windows.
These improvements rarely result purely from material upgrades. Successful sealing strategies increasingly depend on collaboration between seal suppliers, OEMs and end users to understand the true operating conditions equipment experiences in service. Early engagement during equipment design allows seal geometry, gland design and material behaviour to be optimised together rather than treated as isolated decisions.
The value of this collaborative approach can be seen in safety-critical valve applications where sealing performance must be demonstrated under stringent qualification testing. In one flapper valve development programme for the oil and gas sector, advanced thermoplastic sealing materials were selected specifically to eliminate fluid compatibility concerns and rapid gas decompression risks. By combining material expertise with seal design support and precision manufacturing, the valve successfully passed qualification testing on the first attempt, avoiding costly redesign cycles and accelerating deployment.
This collaborative approach matters because the real-world operating environment often differs substantially from nominal specification data. Cleaning chemicals may change over time. Pressure excursions may exceed anticipated levels. Thermal cycles may prove more intense than expected. Without a detailed understanding of those variables, even technically adequate materials may fail prematurely.
Engineering beyond nominal conditions
One of the most persistent misconceptions in industrial sealing remains the assumption that all materials within a given class perform similarly. In reality, the difference between standard and application-specific compounds can be enormous.
Two FKM materials may appear broadly similar on paper while delivering radically different performance under decompression, chemical exposure or thermal cycling conditions. Material formulation, filler selection, cross-linking chemistry and manufacturing processes all influence long-term behaviour under extreme operating conditions. For example, Greene Tweed’s Fusion® 938 is an advanced formulation fluoroelastomer that survives challenging ISO 23936-2 rapid gas decompression scenarios that general purpose FKMs would fail.
This distinction is becoming increasingly important as operators move into more demanding energy transition applications. Hydrogen infrastructure on its own introduces simultaneous challenges involving permeation, cryogenic temperatures, pressure cycling and lubricity. Conventional material selection methods based purely on temperature ratings or basic chemical compatibility tables are no longer sufficient.
Advanced material science is therefore becoming central to future sealing performance. Cross-linked polymers, engineered composite systems and highly specialised elastomer formulations are extending the operational limits of seals under extreme temperatures and pressures. Greene Tweed’s Arlon® 3000XT, for example, is a cross-linked PEEK material capable of operating in conditions beyond the performance range of conventional PEEK alone. Testing has shown that Arlon® 3000XT can demonstrate approximately 40 percent lower creep rates under high-temperature shear loading compared with conventional PEEK grades.
At the same time, digital modelling and predictive engineering tools are beginning to reshape how sealing systems are specified. Finite element analysis and predictive lifecycle modelling increasingly allow engineers to simulate long-term seal behaviour under specific service conditions before manufacturing even begins. This enables designers to evaluate how different material choices are likely to perform over the expected operating life of an asset, providing greater confidence in both engineering decisions and the return on investment of higher-performance materials.
That shift would represent a significant evolution for severe-service equipment design. Instead of reacting to leakage and degradation after installation, engineers could increasingly model how materials behave under pressure cycling, chemical exposure and thermal stress throughout the expected operational life of the asset.
For operators facing growing pressure to improve uptime, reduce emissions and extend maintenance intervals, the importance of reliable sealing technology is only likely to increase. The seal may remain physically small compared with the valve, compressor or pump itself, but in harsh-service environments, it increasingly determines whether the wider system achieves long-term operational reliability or becomes another source of risk, leakage and unplanned downtime. Viewed this way, advanced sealing materials are not simply a premium specification, but a way to reduce the far greater costs of lost production, regulatory exposure, emergency maintenance and avoidable disruption.